Choosing Pulp Equipment for a mill in 2026 requires more than comparing catalogue prices. It demands practical judgment, process knowledge, and honest attention to daily operating conditions. A machine may look efficient on paper, yet struggle with wet bark, inconsistent chips, limited floor space, or unreliable power. Small details matter.
Lars Stenqvist, a recognized pulp technology expert and former Valmet executive, has emphasized, “The best mill investment is not always the biggest machine; it is the system that performs reliably every day.” That principle remains highly relevant. Equipment should match the mill’s wood species, production target, fiber quality, energy strategy, and maintenance skills. It should also support safer operation, lower water use, and measurable environmental performance.
Start with the process, not the brand. Examine debarking losses, chip screening, cooking consistency, washing efficiency, bleaching demand, and recovery capacity. Then review automation, spare-part access, operator training, installation limits, and total lifecycle cost. A low purchase price can become expensive when seals fail, motors overheat, or technicians wait weeks for parts.
There is no perfect selection.
Even experienced teams make assumptions that later prove weak. Pilot testing may reveal unexpected fiber behavior. Local climate can affect storage and corrosion. For this reason, a reliable Pulp Equipment decision combines supplier data, field references, maintenance records, and site-specific testing. The following guide explains how to evaluate these factors and build a more realistic equipment plan for 2026.
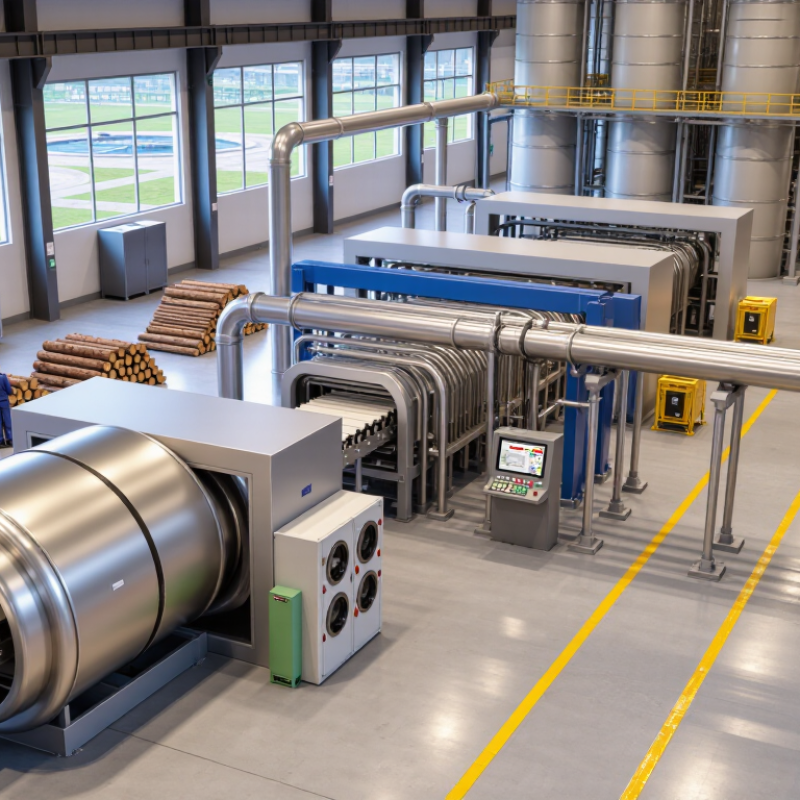
Choosing pulp equipment in 2026 starts with the feedstock, not the machine catalog. Wood species, moisture, bark content, chip size, and contamination directly affect kraft yield. TAPPI technical guidance commonly places kraft pulp yield near 45–55% of oven-dry wood, depending on cooking conditions and lignin removal.
A mill processing 100 tonnes of oven-dry wood may therefore produce about 45–55 tonnes of unbleached kraft pulp. The figure changes with species and target kappa number. Bleaching, screening, and rejects can reduce saleable output further. Reality varies. A spreadsheet can still lie.
Use measured chip samples before sizing digesters, washers, screens, and recovery equipment. Record moisture separately from dry solids. The FAO Global Forest Products Facts and Figures reports wood pulp production and trade using standardized product categories, but local yield calculations need mill-specific testing. Pilot cooking should compare screened chips, oversized chips, and bark-rich material. Poor chip uniformity often creates uncooked knots, higher rejects, and uneven chemical demand.
Equipment capacity should reflect the lower end of the expected range, not an optimistic average. That choice leaves operating room during wet seasons or feedstock changes. It also exposes an uncomfortable question: is the mill maximizing pulp tonnes, or preserving fiber quality? Both goals matter, but they may require different cooking intensity, washing capacity, and recovery margins.
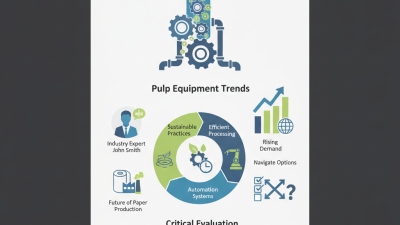
Feedstock selection is a key equipment factor. For conventional kraft pulping, wood commonly produces approximately 45–55% screened pulp yield based on oven-dry wood input. Actual results vary with wood species, chip quality, cooking conditions, and rejects.
Use the lower end of the range for conservative capacity planning. Higher-yield operation generally requires consistent chip size, effective impregnation, controlled cooking, efficient washing, and reliable screening.
Choosing pulp equipment starts with actual mill throughput, not a catalog’s maximum rating. A 500 ADMT/day mill needs equipment sized for steady operation, seasonal fiber changes, and short production surges. A 2,000 ADMT/day mill faces larger flow volumes, higher motor loads, and more demanding maintenance planning. ADMT means air-dried metric tons, so moisture measurement must remain consistent across production records.
Check each process stage separately. Debarking, chipping, screening, washing, refining, and thickening may require different capacity margins. A system rated for 1,000 ADMT/day may struggle if upstream flow regularly reaches 1,200 tons. Allow practical headroom, but avoid excessive oversizing. Large equipment can increase capital cost, energy use, and cleaning time without improving output.
Look beyond nameplate capacity. Review feed consistency, residence time, pressure loss, motor efficiency, spare-part access, and control response. Equipment should handle normal loads without constant throttling. It should also recover safely after brief interruptions. In my experience, a neat spreadsheet can hide awkward realities, especially unstable furnish and delayed maintenance. That deserves honest review. Pilot data, operating logs, and vendor-neutral calculations provide stronger evidence than optimistic guarantees. Ask operators to inspect access points, vibration risks, wash-down areas, and manual tasks before approval. Small details often decide whether rated capacity becomes reliable production.
In 2026, specify the washing system around a measured water balance, not a brochure capacity. A practical design range is 10–20 m³ of water per air-dry tonne (ADT) of pulp. The lower end suits strong counter-current reuse and stable incoming quality. The upper end may be safer for variable furnish or stricter cleanliness targets. Start with a two-week mill survey. Record pulp consistency, filtrate temperature, conductivity, dissolved solids, and carryover at each stage. Small errors here can distort equipment sizing.
Select stages that remove liquor before dilution. Drum or pressure washing can handle high-throughput lines, while presses often improve displacement at higher consistency. Counter-current filtrate flow should move toward dirtier pulp. Fresh water belongs near the cleanest washing point. Keep showers adjustable. A fixed spray rate can waste water during low production. Design pumps, tanks, and screens for the real filtrate load, including start-ups and grade changes. Do not size only for average ADT.
Pilot testing is worth the inconvenience. It reveals foam, fiber loss, plugging, and poor washing that laboratory samples may hide. Track wash loss beside water use. A system using 12 m³/ADT is not efficient if it sends valuable fiber to effluent. Review seasonal water temperature and recovery limits. The target may need revision. That is not failure; it is better engineering. Require accessible sampling points, corrosion-resistant materials, clear control logic, and documented cleaning procedures. Operators should be able to see trends, not guess.
How to Choose Pulp Equipment for Your Mill in 2026?
Assess Recovery Boilers for Over 98% Kraft-Chemical Recovery
A recovery boiler should match your mill’s actual black liquor profile, not a brochure estimate. Start with dry solids, heating value, flow variation, and expected production growth. Measure the basics. These figures influence furnace dimensions, heat transfer surfaces, and chemical recovery stability. A system designed for over 98% kraft-chemical recovery needs accurate liquor control and dependable combustion.
During mill assessments, operators often focus on capacity first. That can be a mistake. Consider steam demand, reduction efficiency, smelt flow, and sootblowing access together. Stable furnace temperature protects recovery performance and reduces avoidable shutdowns. Online monitoring can track oxygen, pressure, temperature, and carryover trends. Small leaks matter. Poor insulation and unstable firing can quietly reduce efficiency.
Safety systems deserve equal attention. Specify reliable interlocks, smelt-water protection, inspection access, and emergency procedures. Emission limits also vary by location, so confirm local requirements before final equipment selection. Over 98% recovery is achievable in a well-operated system, but it is not automatic. Feed quality, maintenance discipline, and operator training remain decisive. I have seen technically strong designs underperform because daily control became inconsistent. That lesson is easy to overlook. Choose equipment that your team can inspect, operate, and improve for many years.
How to Choose Pulp Equipment for Your Mill in 2026?
Select Automation to Keep Kappa Variation Within ±0.5 Points
When selecting pulp equipment in 2026, start with Kappa stability, not maximum production. Kappa measures the lignin remaining after cooking. Automated control can keep variation within ±0.5 points, but only with dependable sampling. That detail matters. In one mill assessment, delayed laboratory results caused overcorrection during chip moisture changes. The operators reacted correctly, but the information arrived too late.
Choose equipment that connects cooking, washing, chemical dosing, and measurement systems. Accurate flow meters and stable temperature sensors support better decisions. Keep control logic simple. A cascade loop can adjust alkali dosing before Kappa drifts widely. An online analyzer should feed both the control system and a clear historian. Operators need to see trends, not just alarms. Alarms should distinguish sensor failure from real process movement.
Do not treat automation as a substitute for maintenance. Poor calibration can defeat expensive control equipment. I have seen a clean-looking dashboard hide a blocked sampling line. The resulting Kappa readings appeared believable for several hours. That experience changed the maintenance checklist. Include routine analyzer verification, sample-line flushing, and backup laboratory checks. Provide a documented manual mode. Use it carefully. The ±0.5-point target should be reviewed across shifts, wood changes, grade changes, and startup periods. Small drift often reveals a larger process weakness.
Practical selection guide for kraft pulp mills: compare process location, measurement capability, automation function, operating range, and control performance before investing in new equipment.
| Process Area | Equipment or Instrument | Key Measurement or Control Variable | Typical Operating Range | Recommended Automation Function | Indicative Control Target | Selection Priority |
|---|---|---|---|---|---|---|
| Wood Preparation | Wood-chip thickness screen and chip-quality analyzer | Chip thickness, oversize fraction, moisture, and bulk density | Chip thickness: approximately 2–8 mm; moisture: commonly 35–55% wet basis | Automatic screening, conveyor interlocks, moisture compensation, and reject monitoring | Stable chip geometry and moisture feed | High |
| Continuous Digester | Cooking temperature, pressure, level, and liquor-flow instrumentation | Cooking temperature, pressure, chip level, white-liquor charge, and H-factor | Temperature commonly about 145–175°C; pressure depends on digester design | Distributed control with cascade loops, feed-forward liquor control, and residence-time management | Kappa variation: ≤ ±0.5 points | Critical |
| White-Liquor Preparation | Causticizing analyzer and lime kiln control package | Active alkali, sulfidity, total titratable alkali, lime availability, and kiln temperature | Active alkali and sulfidity are mill-specific; kiln temperature typically exceeds 900°C | Online titration, ratio control, kiln temperature control, and automatic fuel-air adjustment | Consistent effective alkali charge | Critical |
| Brownstock Washing | Drum or vacuum washer with filtrate-flow and dilution-factor control | Washer dilution factor, filtrate conductivity, consistency, and carryover | Brownstock consistency commonly 10–18% before dilution or screening | Automatic dilution-water control, filtrate routing, shower-flow control, and consistency feedback | Low dissolved-organic carryover | High |
| Oxygen Delignification | Oxygen reactor and alkali-dose control system | Oxygen pressure, alkali charge, temperature, pH, and pulp consistency | Temperature commonly about 90–110°C; pressure commonly about 0.4–1.0 MPa | Multi-variable control using consistency compensation and residual-alkali feedback | Uniform post-oxygen kappa reduction | High |
| Screening and Cleaning | Pressure screen, hydrocyclone, and reject-handling system | Feed consistency, pressure differential, reject rate, and contaminant load | Screen feed consistency commonly 0.8–2.0%; pressure differential is equipment-specific | Automatic reject-rate control, pressure-differential alarms, and staged-cleaner sequencing | Stable fiber recovery and low reject variability | High |
| Bleaching | Bleaching-stage chemical dosing and brightness analyzer | Brightness, pH, residual chemical, temperature, and pulp consistency | Brightness target depends on grade; pH and chemical conditions vary by bleaching stage | Online brightness feedback, chemical-to-kappa ratio control, and stage sequencing | Brightness variation: typically minimized by grade recipe | High |
| Pulp Drying | Pulp-machine moisture, basis-weight, and steam-control system | Basis weight, moisture profile, sheet temperature, steam pressure, and hood humidity | Basis weight depends on product grade; moisture is commonly controlled near the shipment specification | Cross-direction profile control, steam-pressure regulation, infrared or microwave moisture measurement | Uniform moisture and basis-weight profile | High |
| Quality Laboratory | Automated pulp testing and laboratory information interface | Kappa number, brightness, viscosity, consistency, and moisture | Kappa number and viscosity ranges depend on wood species, grade, and process target | Automatic sample identification, calibration tracking, result validation, and historian integration | Fast, traceable quality confirmation | Medium |
| Mill-Wide Automation | DCS, advanced process control, historian, and asset-monitoring platform | Loop performance, process variability, energy intensity, alarms, and equipment condition | Update intervals commonly range from seconds for control loops to minutes for quality analyzers | Model-predictive control, soft sensors, alarm rationalization, predictive maintenance, and digital reporting | Kappa variation within ±0.5 points | Critical |
Note: Operating ranges are representative kraft-pulp industry values and must be validated against the mill’s wood species, production grade, equipment design, chemical balance, and site safety requirements. The ±0.5-point kappa objective is a control-performance target, not a universal operating standard.